 VANTAGE Windows & Doors
 Roofing Industries
 ALTHERM Window Systems
 Dimond Roofing

 Juralco Aluminium
 dormakaba


 Case Studies
 Austaron Surfaces
 Hettich





 Allproof Industries




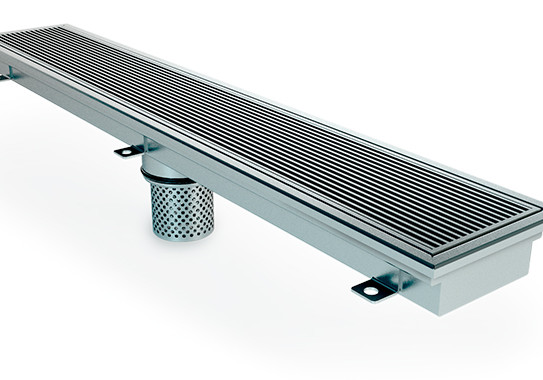

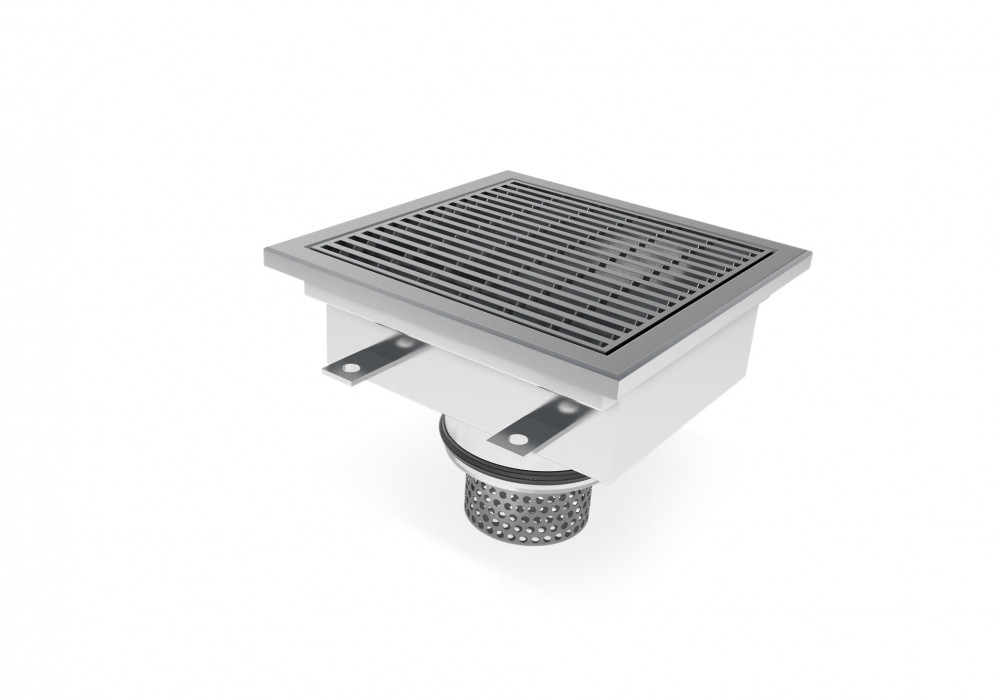


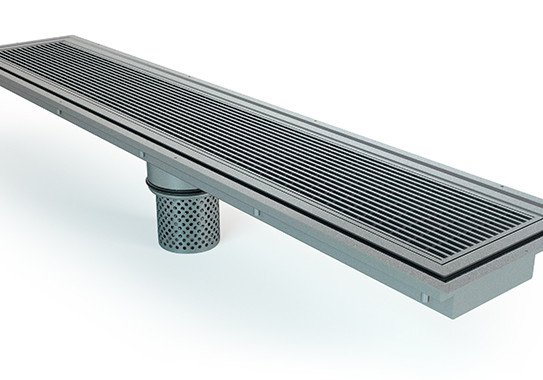
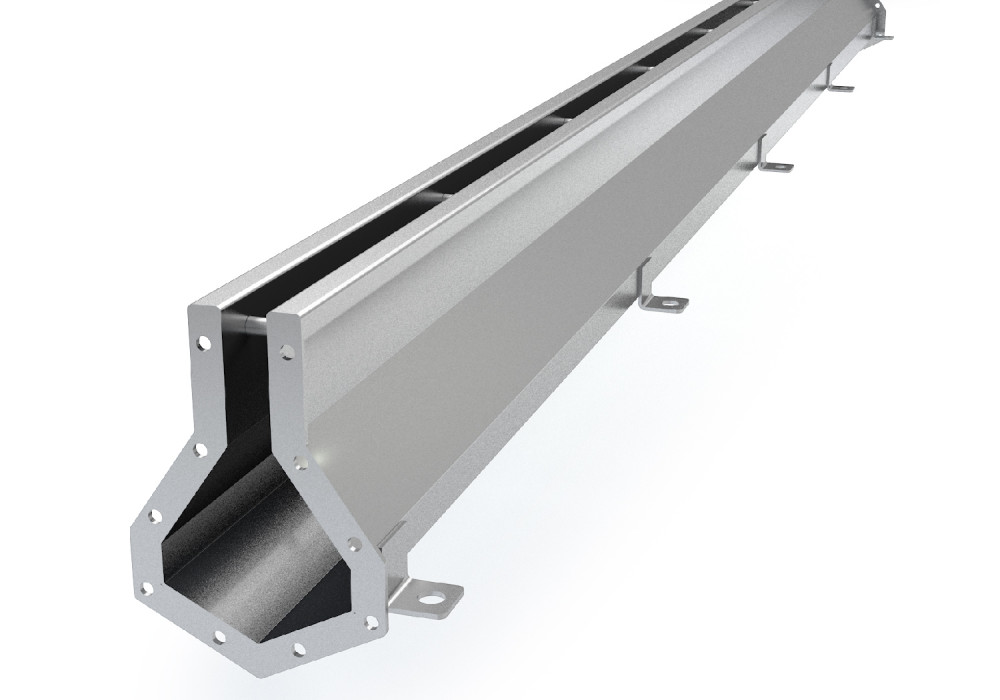

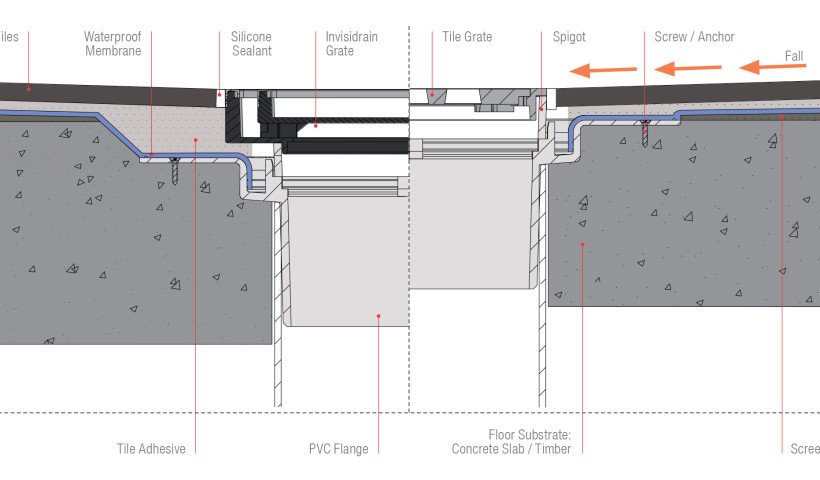
When it comes to food processing and packaging, hygiene is of the highest importance. These areas are controlled by strict cleaning and maintenance regimes to ensure a compliant environment is maintained. A large part of this is managing the trade waste element of the operation, this will ensure that hygiene standards are met throughout the process and that the flooring is kept clean and dry to ensure the safety of the staff.
A recent project that Allproof was requested to assist in was at The Pure Food Co production facility in Auckland. The base build fit-out for their facility had utilised an imported stainless steel floor drain system that was not up to the task. The gratings were slippery and the components not fit for the application which is the processing of fortified foods. The customer was finding that the strainers were filling too often and this was blocking the drains and leaving product on the floor, not in the channels. Regular shutdowns of the lines were required to allow for maintenance and cleaning.
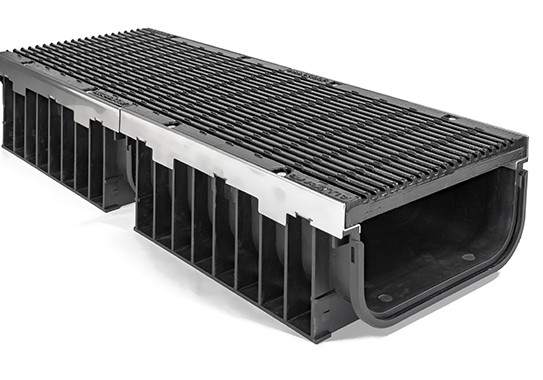
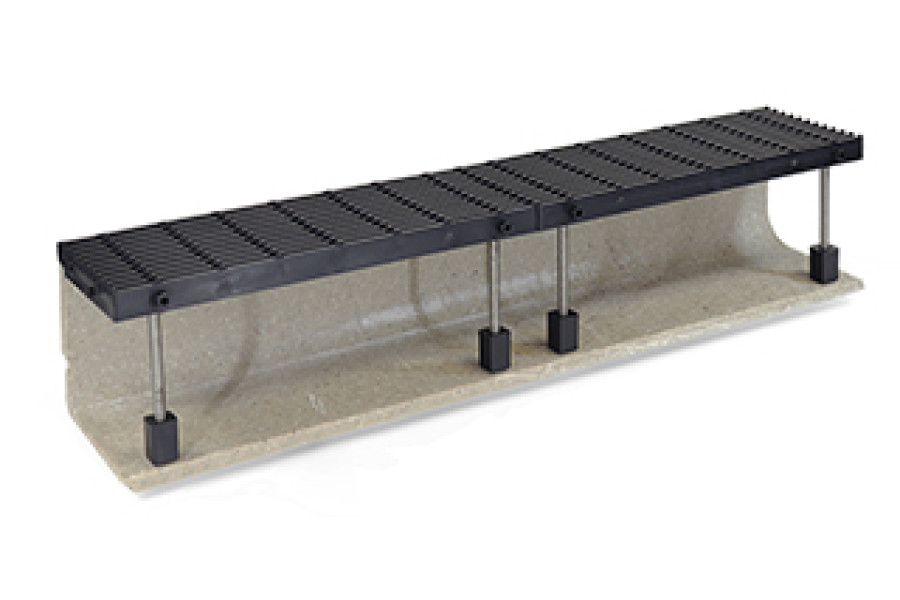
Allproof was engaged to assist with a replacement solution to suit this innovative NZ business’s processing system. The interaction between customer, workers, and manufacturer resulted in a system supplied to site in a timely manner and fit for purpose. The replacement system, made in Allproof’s Toitu accredited manufacturing plant, provided channel drains with wide openings and R13 slip ratings to ensure a durable and safe environment. The strainer baskets were enlarged in the sumps and made easier to service so that the downtime in the cleaning and sterilisation of the area was minimised. The solution was specified, designed, and delivered on time so that the change out of systems caused minimal interruption on their production schedule.
In another project, The Ziwi meat processing plant, the original channel supplier was swapped out to Allproof when it was found that their generic system was lacking for their application. Sizing and slopes in slot drains could be customised, sumps and channels could be detailed as required, not as available. An example of an evolution in design was shown here where the strainer baskets required larger openings so that meat particles could pass through the sumps up to a size of 20mm. Allproof also suggested adding a ‘T’ bar riser to the sump so its location could be more easily identified when it came time for cleaning. The overall design has resulted in a very efficient product to maintain and clean resulting in a well managed hygiene environment.
When it comes to hygiene areas, the design and in-service demands on a drainage system must be of the highest priority. A local manufacturer, with history in the game, will be able to advise on the best product for the application, have multiple and customisable solutions and be able to deliver on their promises in a timely manner. Whether it is healthcare, aged care or an anti ligature drainage required for a secure facility, engaging Allproof at early design stage will ensure all stakeholders are safe, internal processes are streamlined, and the hygiene requirements of the facility are met.
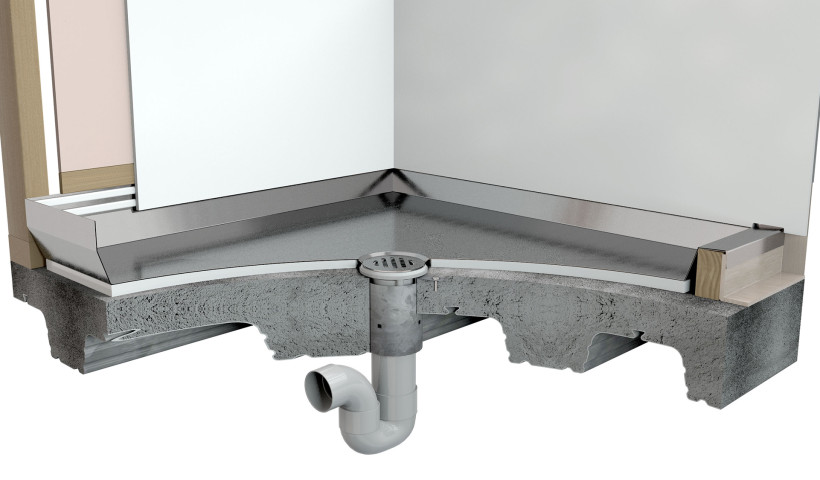
 Popular Products from Allproof Industries
 Posts by Andrew Smith
 Most Popular